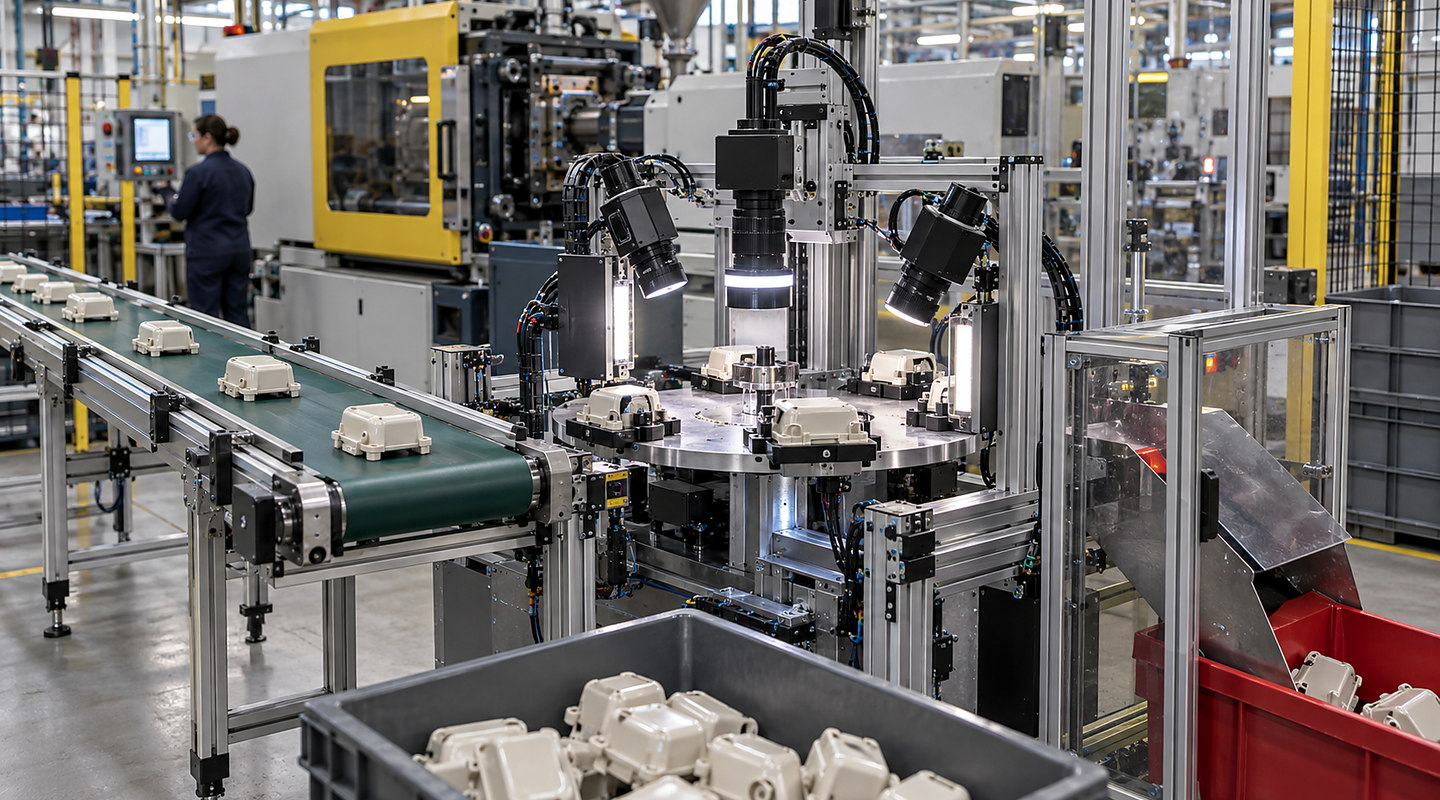
Scratch Detection Systems: How the Process Works
Follow the operating sequence for scratch detection systems, from preparing the input and controlling the main task to handling exceptions and checking results.
Scratch detection compares a controlled image of the surface with an agreed decision about acceptable and unacceptable marks. Define the scratch boundary first, test whether the proposed view reveals it, then link the image result to the correct part and its agreed production response.
The trial should distinguish optical visibility from line integration: a visible scratch in one image does not prove coverage, repeated detection or rejected-part handling. Start with the scratch-definition guide.
Understand the complete route from input to accepted output — Scratch Detection Systems
Plan scratch detection systems around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Follow the material or part through each operating step and include recovery, cleaning and change in the real cycle.
Discuss your application

Four clear stages for scratch detection systems
At each stage, you can review how visible defect or measurement definition for automated surface-scratch detection and false-accept, false-reject and challenge criteria affect the next commitment.
- 01
Define the Visible Decision and Collect Representative Samples
Index acceptable surfaces, unacceptable scratches and borderline examples. Record each expected decision, defect location and direction, finish and relevant batch. Separate the cosmetic acceptance rule from any functional requirement that needs its own test.
- 02
Prove Contrast, Presentation and Timing in an Optical Trial
Compare lighting and viewing arrangements on the same samples. Check scratch direction, edges, curved areas and any areas obscured by the part or fixture. Repeat at the proposed position and movement range; record weak or unseen areas instead of assuming complete coverage.
- 03
Integrate Cameras, Controls, Reject Handling and Recipes
Define how the correct product and finish select the inspection settings, how each image result follows its part and where rejected or uncertain parts go. Agree the response to a missing image, interrupted sequence and restart before the line trial.
- 04
Challenge Marginal Cases and Document Agreed Results
Compare repeated results with the agreed reference decisions. Count missed unacceptable scratches separately from rejected acceptable surfaces, and retain the settings, sample identities and presentation conditions. Document the demonstrated range, exclusions and unresolved cases.
Decisions and results stay connected
| Stage | What happens | What you can review |
|---|---|---|
| Define the Visible Decision and Collect Representative Samples | Confirm the requirements for automated surface-scratch detection, the operating range and the definition of a good result. | An indexed sample list with expected decisions, marked defect locations, surface finishes and unresolved acceptance boundaries. |
| Prove Contrast, Presentation and Timing in an Optical Trial | Compare workable methods using visible defect or measurement definition for automated surface-scratch detection and good, bad and marginal sample range from your real production. | Images and observations from the same samples under each optical arrangement, with the inspected area, weak views and presentation range recorded. |
| Integrate Cameras, Controls, Reject Handling and Recipes | Resolve part presentation and production speed, optics, lighting and environmental conditions and the physical, control, safety and data connections. | The agreed recipe selection, part/result tracking, rejected-part route and missing-image or interrupted-cycle response, including responsibilities at each line connection. |
| Challenge Marginal Cases and Document Agreed Results | Check normal, difficult and fault conditions before your team takes over the system. | Separate missed-defect and false-reject results, repeated-pass conditions, checked production responses, exclusions and actions still needing closure. |
Keep connected responsibilities clear
Your final scratch detection systems scope must also account for recipe, reject and line-control interfaces, false-accept, false-reject and challenge criteria, current regulations and the conditions at your site.
- A camera can only assess a property made visible and repeatable by the inspection setup.
- Sample diversity and marginal cases determine how meaningful a feasibility result is.
- Visual inspection does not replace hidden, destructive, functional or statutory tests.