Mechanical
Confirm datums, loads, envelopes, transfers, guarding and service access around in-line inspection using automated surface-scratch detection.
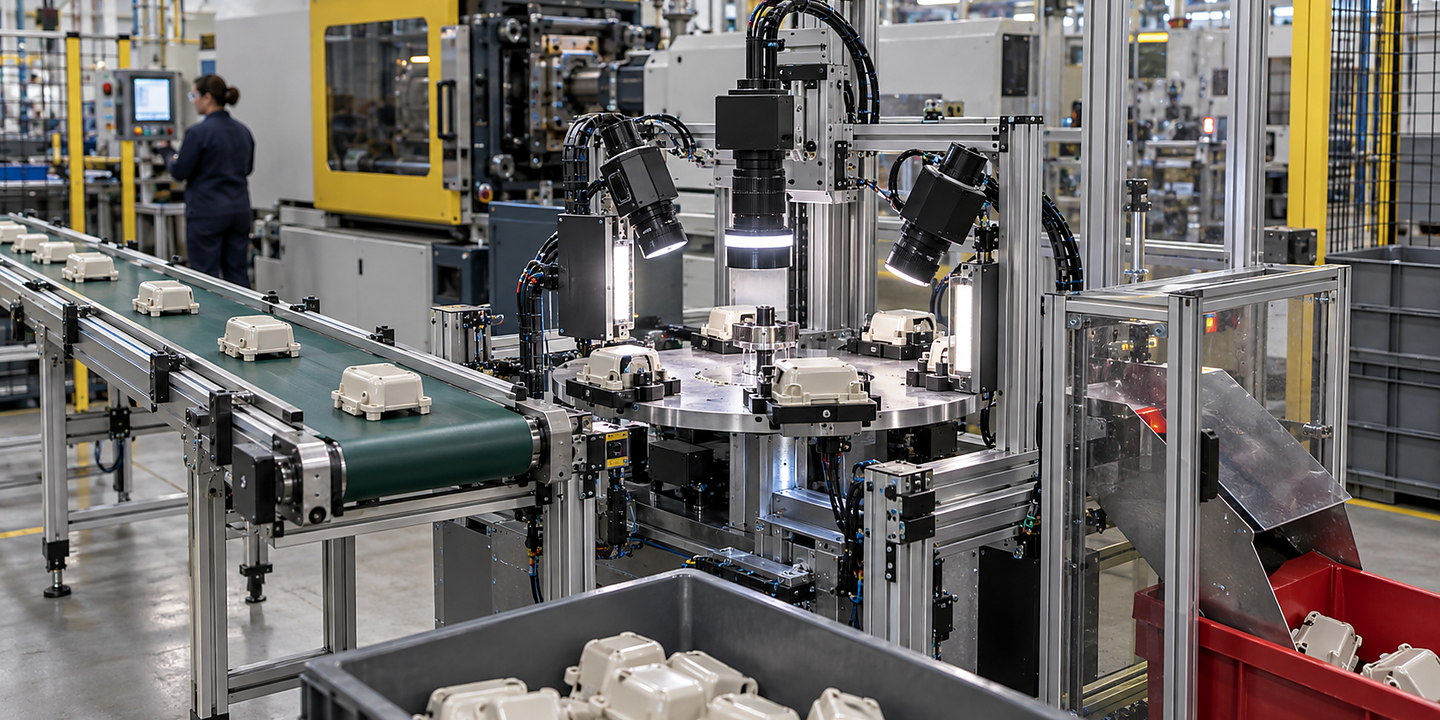
Plan mechanical, electrical, control, data, safety and operator interfaces for scratch detection systems.
Define where the required surface is visible and associate each inspection result with the correct part. Agree image timing, recipe changes, reject handling and the response to an uncertain image or missing result.
For retrofit or multi-variant checks involving automated surface-scratch detection, define every physical connection, signal, responsibility, check and fallback before installation.
Plan scratch detection systems around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Your integration review should connect part presentation and production speed, optics, lighting and environmental conditions and the people who run the process.
Discuss your application

Confirm datums, loads, envelopes, transfers, guarding and service access around in-line inspection using automated surface-scratch detection.
For Scratch Detection Systems, list the supplies, isolation, protective devices, panels and cable routes required by the proposed installation.
Agree operating modes, line handshakes, permissives, faults, recovery and recipes affected by recipe, reject and line-control interfaces.
Review risk controls, stop behaviour, access, reset and the checks needed around optics, lighting and environmental conditions.
Define identifiers, timestamps, results, retention and recovery needs for false-accept, false-reject and challenge criteria.
Plan normal operation, replenishment, clearance, cleaning, maintenance and training for retrofit or multi-variant checks involving automated surface-scratch detection.
For Scratch Detection Systems, your team can review each stage before the complete installation is put into routine use.
Share representative good, bad and marginal samples, including the normal range for visible defect or measurement definition for automated surface-scratch detection and the difficult good, bad and marginal sample range cases.
Compare suitable methods and use focused trials to show how each option performs against part presentation and production speed.
Connect the equipment to your line, services and controls while resolving optics, lighting and environmental conditions for day-to-day operation.
Confirm recipe, reject and line-control interfaces, then complete and record false-accept, false-reject and challenge criteria before your operating team takes over.
For your application: check part presentation and production speed, optics, lighting and environmental conditions, recipe, reject and line-control interfaces, and false-accept, false-reject and challenge criteria as part of the complete line trial.